
Ready to automate your workflow?
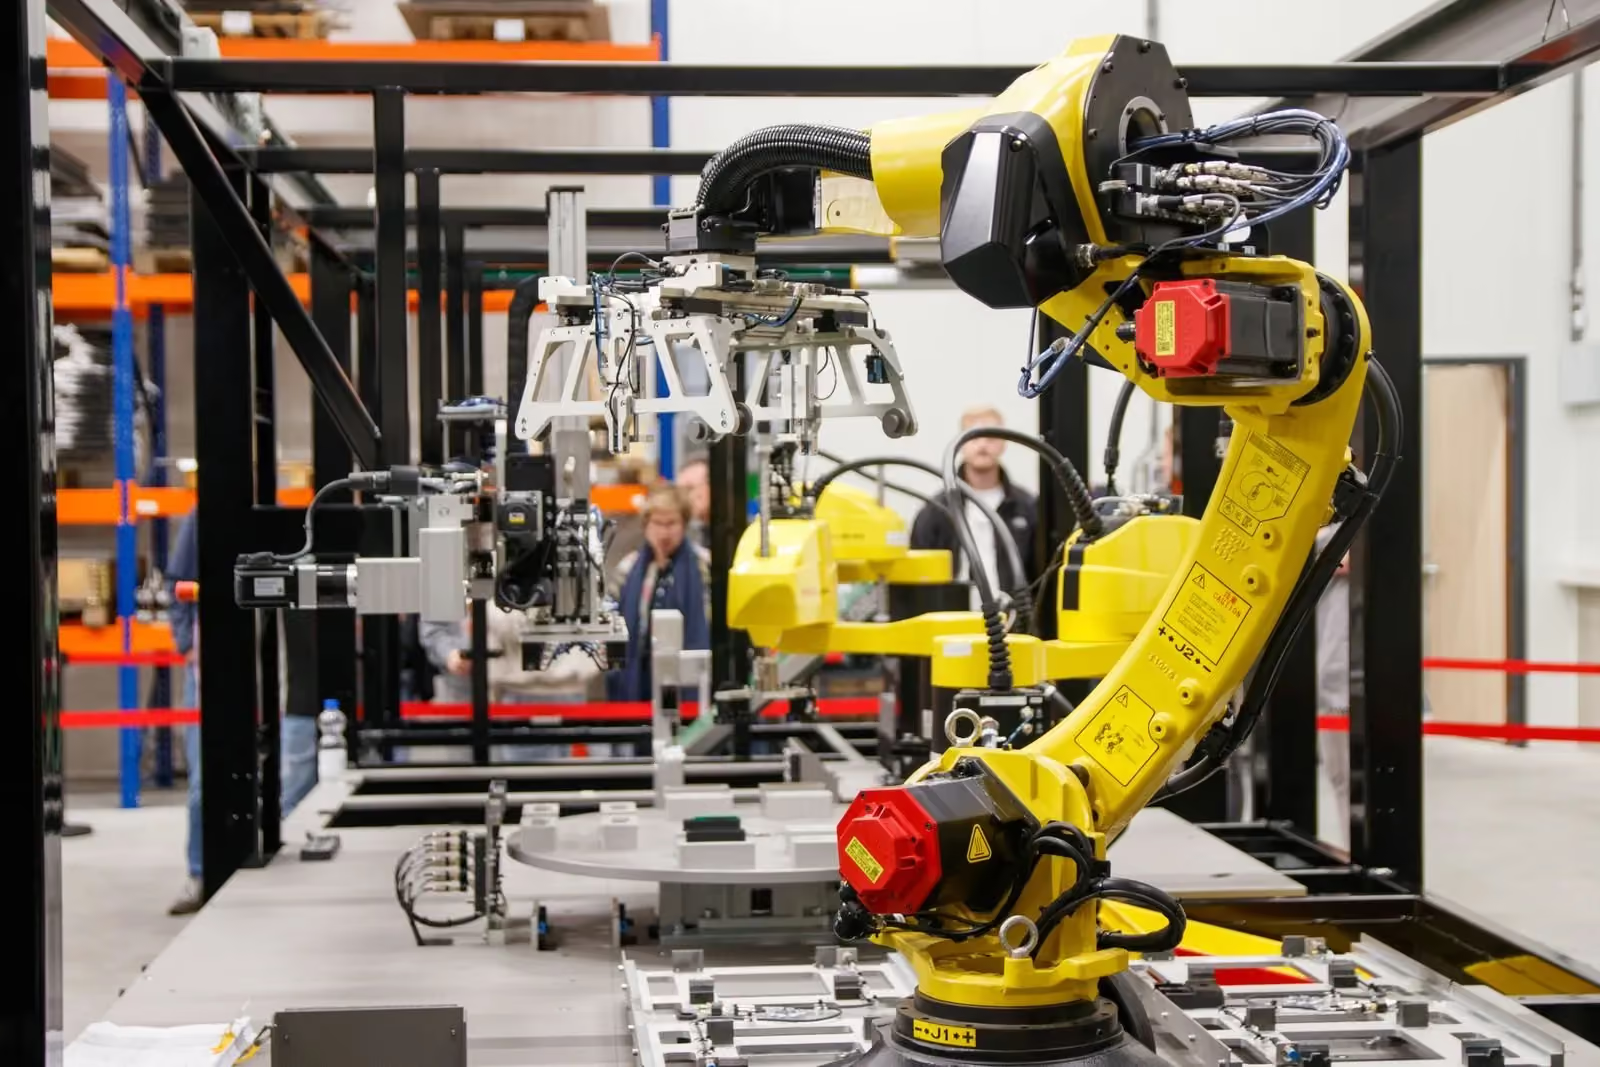
When a station is specified, the first number people reach for is the robot's repeatability. It is printed on the datasheet, it is small, and it feels like the answer. It is rarely the question.
The tolerance a station has to hold is set by whatever has to find the part next. Placement tolerance is inherited, and getting it right means starting downstream and working back, not starting with the arm.
Ask what comes next
A pick-and-place station is judged by the station after it. If the next tool needs the part within half a millimetre to find it, that half-millimetre is the spec, whatever the robot's datasheet says it can do.
So we start from your process sheet, not from our catalogue, and take the tolerance of the next operation as the figure this station has to hold. Where there is no process sheet, we measure what the next station actually tolerates by trial, and write it down.
The datasheet tells you what the robot can do. The next station tells you what it has to.
Where the error actually comes from
Robot repeatability is rarely the limit. In most stations it is one of the smallest contributions to the total. We budget every source of error separately and show the sum before the design is fixed:
- Part variation from batch to batch, taken from your sample rather than the drawing;
- Fixture seating — how the part sits before it is picked, and how much that moves;
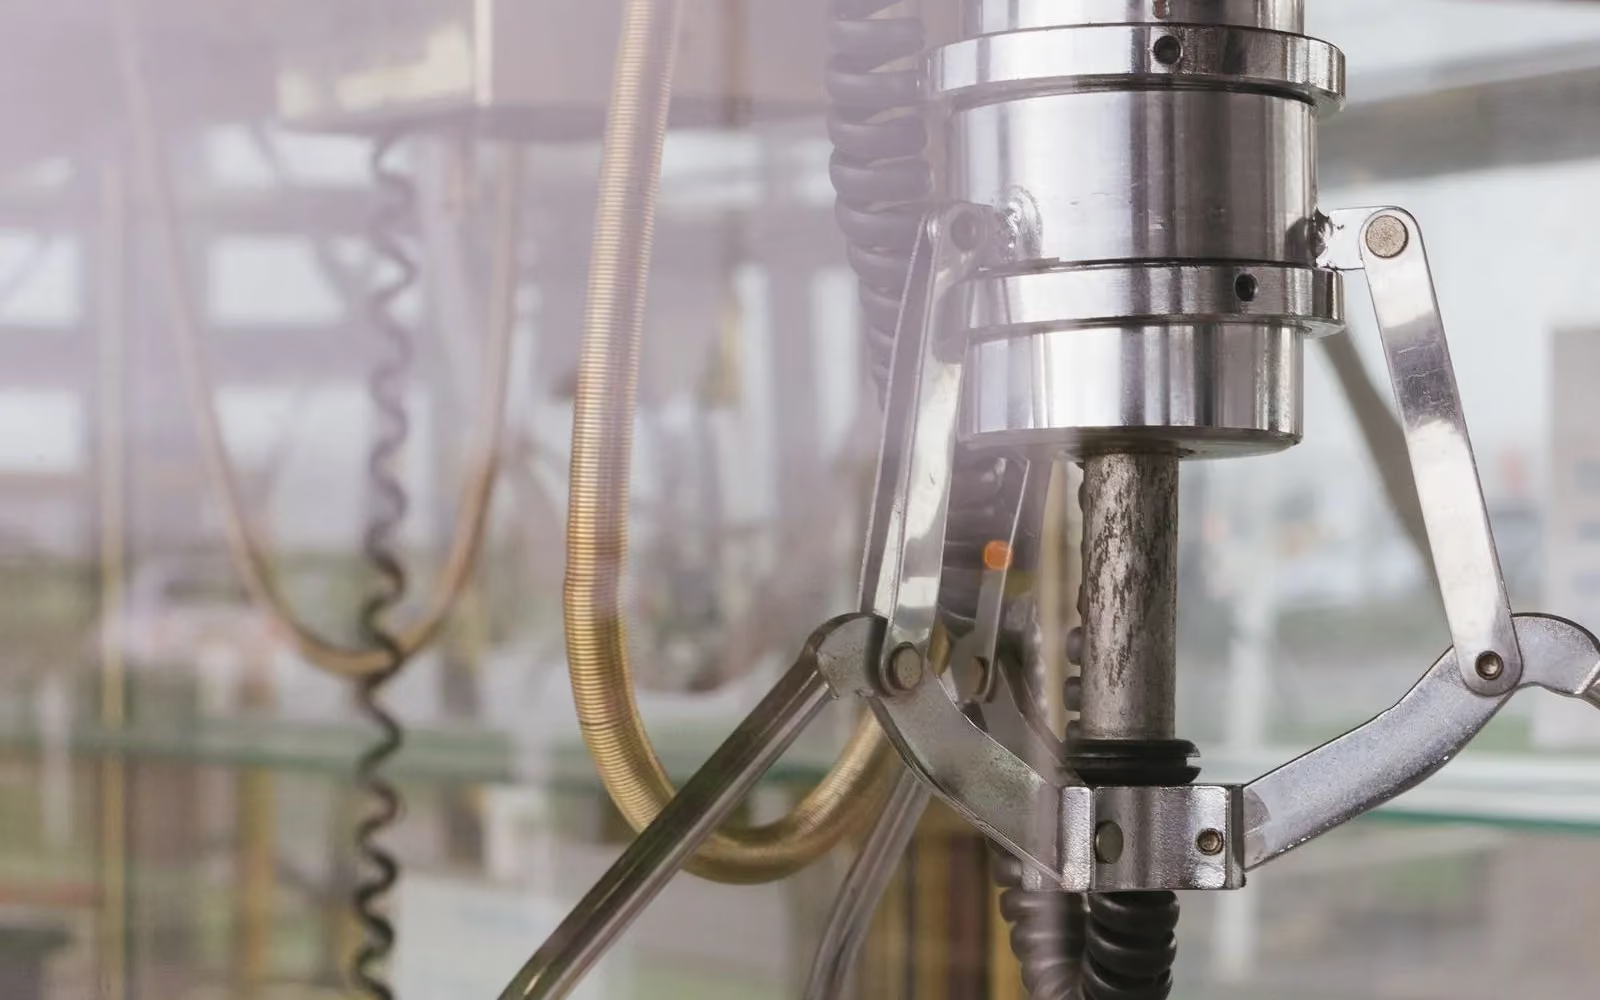
- Jaw wear over the service interval, not only on day one;
- Arm repeatability at the speed and payload the station actually runs.
In most stations the first three add more than the fourth. That is why a more expensive robot so rarely fixes a tolerance problem.
Budget for the worst day, not the first
A new gripper on a fresh fixture with a good batch of parts will hold almost anything. The station has to hold the tolerance on the last day of the service interval, with worn faces, a batch at the edge of its drawing and a fixture that has taken a few knocks.
So each item in the budget is taken at its worst credible value, not its typical one. If the sum still closes, the station will hold its number for its whole life, not only for its acceptance test.
Closing the budget
When the sum does not close, the fix is usually cheaper than people expect. In order of how often we use them:
- add a locating feature to the fixture so the part seats the same way every time;
- change the contact faces so the jaws centre the part as they close;
- add a check station or a vision correction before the hand-off;
- only then, look at a more repeatable arm.
Say it before the order
Whatever the fix, it is agreed before anything is cut. A tolerance problem found at commissioning costs a redesign and a second shutdown. The same problem found in the budget costs a conversation and a line on a drawing.
Final thoughts
Start from the next station, budget every source of error at its worst, and close the gap with the fixture and the faces before reaching for the robot. Stations specified that way hold their number long after the acceptance test is forgotten.


